
-
E-mail
-
WhatsApp & WeChat
WhatsApp & WeChat
 Blister Packaging Line
 Automatic Counting Machine Line
 Liquid Filling Machine Line
 Powder Filling Machine Line
 Granule Filling Machine Line
 Bag Packing Machine
+86 151 6187 8967
Capsule Counting Machine
Accuracy above 99.9% on a capsule counting machine comes from how the capsules are fed, how clean the sensing lenses stay, and where the room's relative humidity sits. It does not come from fitting a fourth sensor. In nearly every miscount complaint I have been called to, the detector was working correctly on the wrong input. This is the sequence I use on site: pick the sensing technology that suits your shell, remove the failure modes that actually cause miscounts, then prove the number with a challenge test.
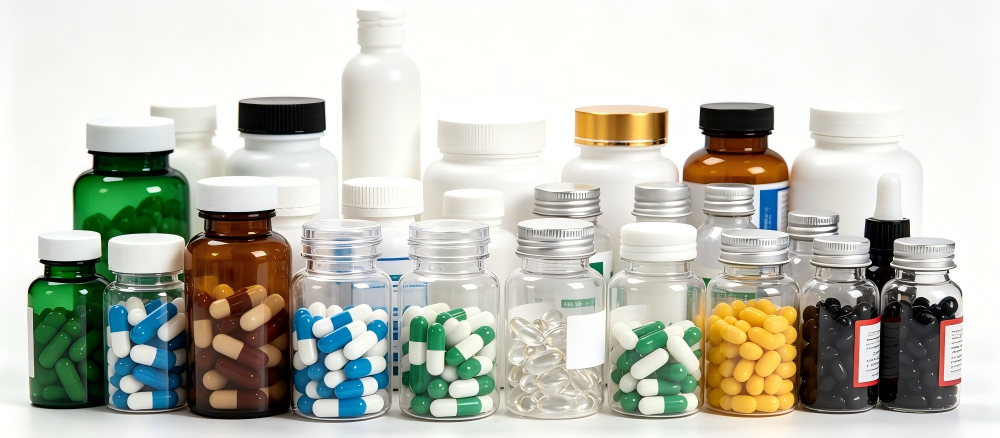
Capsule Counting Machine
Most buyers ask which sensor on a capsule counting machine is the most accurate. The better question is which one drifts slowest in your dust. A through-beam photoelectric array counts interruptions of an infrared beam: fast, cheap, and the first thing to lose calibration when polishing talc films the lens. A machine-vision head reads a full frame per capsule and can be trained on banded or printed shells, but it costs two to three times as much and needs its own window-cleaning discipline.
| Technology | Capsules/h | Size range | Dust sensitivity | Cost ratio | Best fit |
|---|---|---|---|---|---|
| Through-beam photoelectric array | 30,000–90,000 | 000–5 | High: lens film shifts the threshold in one shift | 1.0 | Opaque shells, few SKUs |
| Machine vision with image processing | 20,000–70,000 | 000–5, printed | Moderate: sealed window, heavy dust still degrades | 2.2–3.0 | Banded capsules, high SKU count |
| Mechanical rotary disc counter | 6,000–25,000 | 00–3 | Low for sensing; jams on tacky product | 0.4–0.6 | Supplements, tight budgets |
Two things I flag during selection. Vendors quote capsules per hour using size 0 hard gelatin in a clean batch, so ask for that figure re-quoted on your smallest capsule and your dustiest product. And a vision head only earns its premium when SKU count and changeover frequency are high.
Capsules misbehave differently from tablets in every way that matters here: they are light, they bounce, and they carry charge.
HPMC shells, and gelatin to a lesser degree, pick up charge as they tumble down a stainless channel. Below roughly 40% RH the surface resistivity climbs and capsules cling to the channel wall and to each other. Two that cling together through the sensing plane are read as one; one that clings at the gate and releases late lands in the next bottle. I specify 45–55% RH in the counting room, ±5%, as a machine utility rather than a facilities afterthought. In a Gulf plant that means humidification against a 24 °C supply air setpoint; in Southeast Asia it more often means dehumidification, because ambient sits at 70–80% most of the year.
If shells are polished with talc or magnesium stearate, some of that becomes airborne at the counting head. On a photoelectric array the film lifts the baseline and flattens contrast, so accuracy is fine at 08:00 and marginal by the end of second shift. On one audit job we recorded a 0.4 percentage-point fall in exact-bottle rate across a single eight-hour shift on a talc-polished product. Moving polishing upstream and adding extraction removed most of it.
Almost every counting complaint I have diagnosed was a feed problem wearing a sensor costume. Hold the hopper bed between roughly 30% and 70% with a vibrating fork or capacitive probe, because a deep bed compacts and bridges while a low bed starves and then surges. Use a two- or three-stage vibratory cascade with independent amplitude per stage, typically 40–80% of maximum, tuned so the last stage delivers a single-file stream rather than a ribbon. Fit a servo cut-off gate: a pneumatic gate at 40–60 ms throws in a trailing capsule on every cycle. Extract at the feed point at 150–300 m³/h per head and about 0.5 m/s capture velocity, balanced so it removes airborne talc without lifting capsules out of the channel.
A spec-sheet figure means nothing without a protocol. This is the one I run at FAT and repeat at OQ, on the customer's own capsules and on their worst batch rather than a clean sample.
| Test | Setup | Acceptance |
|---|---|---|
| 100-count challenge, n = 30 | Thirty consecutive bottles, hand-counted by two operators | At least 29 exact; deviation never more than one capsule |
| 500-count challenge, n = 10 | Bulk containers, cross-checked on a 0.01 g balance | All within ±1 count, i.e. not worse than 99.8% |
| Defect rejection | Twenty known defects seeded into 10,000 good capsules | At least 19 diverted to a locked, reconciled reject bin |
| In-process check | Written into the SOP and forced by the HMI where possible | Every 30 minutes per head, plus at start-up and after stops over five minutes |
The number buyers misread. A per-capsule accuracy of 99.9% does not mean 99.9% of bottles are correct. On a 30-count bottle it is 0.99930, so about 97.0% of bottles are exact. To get 99.5% of bottles exact you need roughly 99.98% per capsule. Always ask a vendor whether the quoted accuracy is per capsule or per container.
Qualification follows the IQ/OQ/PQ structure of EU GMP Annex 15, with challenge tests in OQ and drift data in PQ. Where the control system holds recipes and batch records, Annex 11 covers the computerised system, and for supply into the US, 21 CFR Part 11 governs electronic records and signatures: unique user IDs, an audit trail recording who changed a setpoint and when, and a batch report that cannot be edited afterwards. The drug CGMP obligations sit in 21 CFR 211. On the machine side I ask for a CE declaration under Machinery Regulation (EU) 2023/1230, which replaces Directive 2006/42/EC, supported by a risk assessment to EN ISO 12100 and electrical safety to EN 60204-1. ISO 13485 matters only if the line also makes a medical-device combination product.
These are the bands I quote when a buyer asks what a capsule counting machine will hold on a real floor. All figures are size 0 and size 1 hard gelatin at 30-count.
| Configuration | Capsules/h | Bottles/min | Per-capsule | Exact-bottle | Rejects | Changeover |
|---|---|---|---|---|---|---|
| 8-channel array, single head | 36,000 | 20 | 99.7% | 91.4% | 0.6% | 35 min |
| 12-channel array, servo gates | 60,000 | 33 | 99.9% | 97.0% | 0.3% | 22 min |
| Vision head, 16 lanes | 84,000 | 46 | 99.95% | 98.5% | 0.2% | 12 min |
| Twin vision heads, two-up | 150,000 | 83 | 99.95% | 98.5% | 0.25% | 18 min |
A packer running hard gelatin sizes 0 and 1 plus one HPMC line, three shifts six days a week, called us in at 60-count HDPE bottles against 34 bottles per minute. What failed first was not the counter. The plant ran a chilled-water air handling unit with no humidification, so in the dry season the room fell to 32–35% RH and capsules clung in the channels before releasing in pairs. Polishing happened in the same room, so the lens window filmed within a shift, and the gate-to-neck drop was 210 mm, visibly bouncing the size 1 product.
We changed four things and left the detectors alone. Humidification now holds 50% ±5% RH. Polishing moved upstream behind a deduster with 250 m³/h of extraction at the head. Drop height went to about 95 mm with an anti-bounce deflector. Lens cleaning became a per-shift item with 70% IPA, and recipes were locked behind operator-level access. Measured over two weeks either side: miscount-driven rejects fell from 1.9% to 0.35%, the exact-bottle rate rose from 93.1% to 97.6%, OEE moved from 61% to 74%, and changeover dropped from 40 minutes to 24.
Spec-sheet speed is the obvious trap; the expensive ones are quieter. Change parts get quoted for the two sizes in the enquiry, not the two you add in year two. FAT runs on your best capsules rather than your worst, which hides feed surging. Spare lens sets are left off the order, so one scratched window becomes a six-week wait. Validation documentation arrives in the builder's language only and stalls an EU or PIC/S audit by a month. Put ambient into the enquiry too: 220–240 V at 50 Hz is standard across Southeast Asia and the Gulf, but a 34 °C room at 75% RH is not the same duty as 21 °C in Germany.
How accurate is a capsule counting machine in real production?
Per capsule, a well-set line sits at 99.9% or better. What matters commercially is the exact-bottle rate, which on a 30-count bottle is about 97% at that per-capsule figure. Ask for both numbers and for the protocol behind them.
Can one machine handle gelatin and HPMC shells?
Yes, as separate recipes. HPMC carries more charge and has different surface friction, so channel amplitude and gate timing need retuning and the humidity window matters more. Expect 5–10% lower speed on HPMC.
What room conditions do I need?
Hold 45–55% RH at the counting head and 20–24 °C. Below 40% you fight static; above 60% with hygroscopic fills you fight shell softening and clumping. Specify it as a utility.
How often should sensors be cleaned?
Once per shift for a talc-polished or dusty product, weekly for a clean, unpolished one, and log it. The drift is gradual enough that nobody notices until the in-process check fails.
What documentation should come with a capsule counting machine?
IQ/OQ/PQ protocols and reports built on EU GMP Annex 15, a computerised-system package meeting Annex 11 and 21 CFR Part 11 if you supply the US, material certificates for product-contact parts, a CE declaration under Machinery Regulation (EU) 2023/1230, and English-language manuals and wiring diagrams.
How many change parts do I need per capsule size?
One channel set, one gate set and one funnel per size, plus a second channel set for your highest-volume size, because that is the part that wears and gets dropped during cleaning.
Written by Helen Xu | Chief Industrial Application Engineer
Helen Xu is a Chief Industrial Application Engineer with 9 years of specialized experience in packaging machinery and liquid filling machine design, equipment model selection, and full production line process optimization. He focuses on delivering customized packaging & filling solutions for pharmaceutical, food, and chemical manufacturing industries, with mature practical expertise in GMP compliance, ISO 9001 quality management standards, and turnkey large-scale filling & packaging production line integration.
E-mail Us
Chat With Us


